SGS Laboratory
every phaseindependent test
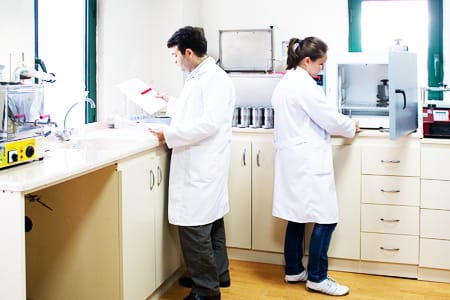
An in-house SGS laboratory; trained staff run checks at every stage of production.
An SGS laboratory runs inside the Çorlu factory. It is staffed by trained specialists, and checks are carried out at every stage of production; greige fabric, dyehouse and finishing phases each pass control on their own before the lot moves on.
This laboratory is distinct from the colour-matching laboratory. Where colour matching gets the shade right, here conformity is verified in the independent, accredited language of testing. We measure each phase on its own terms; one stage does not blindly inherit the output of the last.
We keep control next to production, on the floor, for a simple reason. Caught early, a deviation is stopped early; we know whose hands and which shift produced a result, and we keep the record. What ships is the measured fact, not a claim.
| Location | On-site (Çorlu) |
|---|---|
| Facility | SGS laboratory |
| Scope | Independent check at every production phase |
| Staff | Trained specialists |
| Focus | Independent / accredited conformity testing |
Related guides: Knit Quality Testing: What to Measure in Polyester · Microplastics: Fibre Shedding and Control · Digital Product Passport (DPP) & ESPR: What It Means for Textiles
Questions about this unit
Is «bursting ≥ X kPa» enough in a specification?
No, because the test area changes the result directly: measured over 7.3 cm² instead of 50 cm², the same fabric returns a higher kPa simply because the smaller area contains fewer weak points. The area (preferably 50 cm² for knits) and the method — hydraulic ISO 13938-1 or pneumatic ISO 13938-2 — must therefore be fixed together. The result is reported as kPa alongside distension in mm.
From the guide: Knit Quality Testing: What to Measure in Polyester
Is «C06 ≥ 4» a complete fastness criterion on its own?
No, the variant code is missing. ISO 105-C06 offers several wash severities, and the code defines the temperature (A = 40 °C, B = 50 °C, C = 60 °C), the number of steel balls (1 = none, 2 = one ball) and whether bleach is included (S = standard, M = with bleach). Colour change is also graded on the grey scale SEPARATELY from staining onto the multifibre adjacent strip; on deep, bright disperse shades wet crocking (X12 wet) is usually the hardest item to pass.
From the guide: Knit Quality Testing: What to Measure in Polyester
What most determines microfibre shedding?
The polymer itself (PET, nylon, viscose) is SECONDARY; what decides is the STRUCTURE. Fibre breakage is essentially mechanical: the friction, bending and tension cycles in a washing drum pull fibres out of the yarn body. The strongest variable is yarn morphology — staple yarns carry countless short fibre ends that friction draws out easily, while continuous filament yarns have almost none. Finishes that raise a heavy nap also increase shedding.
How is shedding measured?
The ISO 4484 series is the backbone of the field, and the choice of method is NOT open to interpretation. ISO 4484-1:2023 determines the mass loss in washing gravimetrically (mg/kg) — ideal for comparing fabrics against one another and selecting low-shedding structures. ISO 4484-2:2023 then qualitatively confirms whether the collected sample really is plastic. Mitigation is most effective at source; on end-of-machine filters, independent measurements have reported reductions of about 78% for XFiltra and about 80% for Lint LUV-R by mass.